
Blog
Why a Planned Spare Parts Strategy Protects Industrial Production Uptime

Downtime Costs Drive a New Focus on Spare Parts
In industrial production, few events are as disruptive as an unexpected machine stoppage. When a key line halts, the impact spreads quickly through scheduling, logistics, labor planning and customer commitments. Lost output is only part of the cost. Overtime, expedited shipping, scrapped material and damaged customer confidence can add significantly to the total. Because of this, many manufacturers are taking a fresh look at how they manage spare parts for their automation systems. In the past, spare parts were often treated as an afterthought, handled by whoever had time to place an order when something failed. Today, more companies view spare parts management as a core element of operational resilience. They recognize that the availability of a single controller, drive or circuit board can decide whether a breakdown lasts an hour or several weeks. This shift in thinking has encouraged closer cooperation between maintenance, engineering and purchasing teams. Together they evaluate which components are most critical, how long replacements take to obtain and what level of stock offers the right balance between cost and protection. The goal is not to hold every possible part, but to make sure the right parts are available when they are truly needed.
Identifying Critical Components
A sound spare parts strategy begins with a clear understanding of which components matter most. Not every part carries the same risk. Engineers typically start by mapping the equipment on each production line and assessing how a failure would affect output, safety and quality. Components that have no redundancy, that are difficult to source or that sit at the heart of the control system are usually classified as critical. Examples include programmable controllers, servo amplifiers, main control boards, specialized drives and key safety devices. Other items, such as standard terminals or common relays, may be readily available from many sources and therefore require less stock. Failure history is another important input. Parts that have failed repeatedly, or that operate under high thermal or mechanical stress, deserve special attention. Maintenance records, alarm logs and technician experience all help build an accurate picture. Once critical components are identified, teams can document exact part numbers, revision levels and compatible alternatives. This information becomes the foundation for stocking decisions and supplier discussions. Without it, purchasing teams may order the wrong items or spend valuable time searching for details during an emergency, when every minute of downtime adds to the cost.
Balancing Inventory Investment and Risk
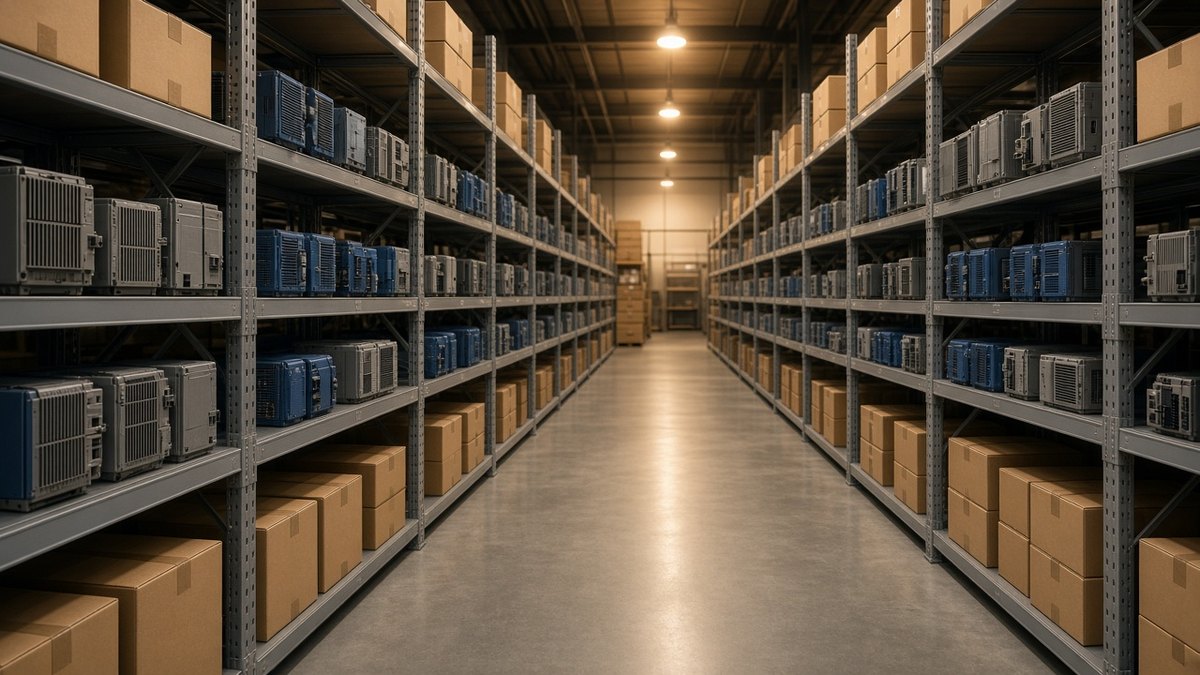
Holding spare parts ties up capital, occupies storage space and requires careful handling, especially for sensitive electronics. At the same time, the absence of a key part can be far more expensive. Finding the right balance requires a thoughtful approach. Many plants now apply risk-based stocking, where inventory levels reflect both the likelihood of failure and the consequences of a stoppage. High-impact components with long lead times may justify keeping units on the shelf, while low-impact items can be sourced when needed. Some manufacturers share spare parts across several sites, creating a central pool that reduces duplication while maintaining protection. Others work with specialized suppliers who hold stock on their behalf and commit to rapid delivery. Storage conditions also matter. Electronic modules should be kept in clean, dry environments, protected from static discharge and periodically checked to ensure they remain ready for use. Regular reviews help keep inventory relevant, because equipment changes over time and obsolete stock can accumulate unnoticed. By treating spare parts as a managed portfolio rather than a static collection, companies can control costs while still being prepared for the failures that inevitably occur in complex automated systems.
The Challenge of Obsolete Automation Hardware
Obsolescence ranks among the most pressing issues in spare parts management. Automation manufacturers regularly introduce new product generations and gradually withdraw older models from production. For factories that rely on equipment designed around those older models, this creates a growing challenge. Original replacement parts become harder to find, lead times lengthen and prices may rise as supply dwindles. Plants that do not plan ahead can find themselves facing extended outages because a single discontinued component cannot be replaced quickly. To manage this risk, maintenance teams monitor lifecycle announcements and assess which installed products are approaching the end of active support. They then decide whether to purchase additional spares, identify compatible alternatives or plan a migration to newer technology. Specialized suppliers of legacy automation parts play an important role during this period, as they can locate tested units that are no longer available through standard channels. Careful verification of condition, part numbers and firmware versions is essential to avoid compatibility issues. Over the long term, obsolescence planning should be built into equipment strategy from the beginning, so that every major purchase considers how parts will be supported throughout the expected life of the machine.
Building Strong Supplier Relationships
Even the best internal planning depends on reliable external partners. Plants increasingly look for suppliers who understand industrial automation, can identify parts accurately and respond quickly when urgent needs arise. A strong supplier relationship goes beyond simple transactions. It includes open communication about stock availability, realistic delivery estimates and clear information about product condition. Suppliers who inspect components before shipment, package them carefully and provide traceable documentation help maintenance teams work with confidence. Many manufacturers now maintain a shortlist of trusted sources for different categories of equipment, such as controllers, drives, motors, sensors and power components. Having established accounts and agreed procedures in place saves valuable time during emergencies, when approvals and paperwork can otherwise delay critical purchases. Some companies also hold periodic reviews with key suppliers to discuss upcoming risks, obsolescence trends and potential stock commitments. These conversations allow both sides to prepare in advance. In a market where demand for automation components can change quickly, a cooperative relationship can be the deciding factor that ensures a replacement arrives on time. Ultimately, supplier partnerships extend the capabilities of the maintenance team and strengthen the overall resilience of production operations.
Keeping Records Accurate and Accessible
A spare parts strategy is only as good as the information behind it. Many plants discover that their records are scattered across spreadsheets, paper files and the memories of individual technicians. Consolidating this information into a single, well maintained register makes a real difference. Each entry should describe the component, where it is installed, its exact part number and revision, the quantity held in stock and the preferred sources for replacement. Storage locations should be clearly labeled so that parts can be found quickly during a night shift or weekend call-out. When a spare is used, the record must be updated and a replacement ordered without delay. These routines may appear simple, yet they prevent the frustrating situation in which a part is believed to be in stock but cannot be located when it is urgently needed.
From Reactive Buying to Planned Reliability
The move from reactive buying to planned spare parts management reflects a broader change in industrial maintenance culture. Instead of accepting breakdowns as unavoidable surprises, manufacturers are building systems that anticipate them and limit their impact. A planned strategy brings together asset knowledge, risk assessment, inventory control, obsolescence monitoring and supplier cooperation. Each element supports the others. Accurate equipment records make stocking decisions easier, and good supplier relationships reduce the amount of stock that must be held on site. Regular reviews keep the strategy aligned with changing equipment and production priorities. The benefits extend beyond reduced downtime. Maintenance teams experience less stress during failures, purchasing departments avoid costly emergency orders and production planners gain greater confidence in their schedules. Customers ultimately benefit from more consistent deliveries and stable quality. As automation becomes ever more central to manufacturing, the importance of spare parts management will continue to grow. Factories that invest time and attention in this area today are building a foundation of reliability that supports competitiveness for years to come. In a demanding industrial environment, being prepared is often the most cost effective decision a manufacturer can make.